What Is Lanthanated Tungsten?
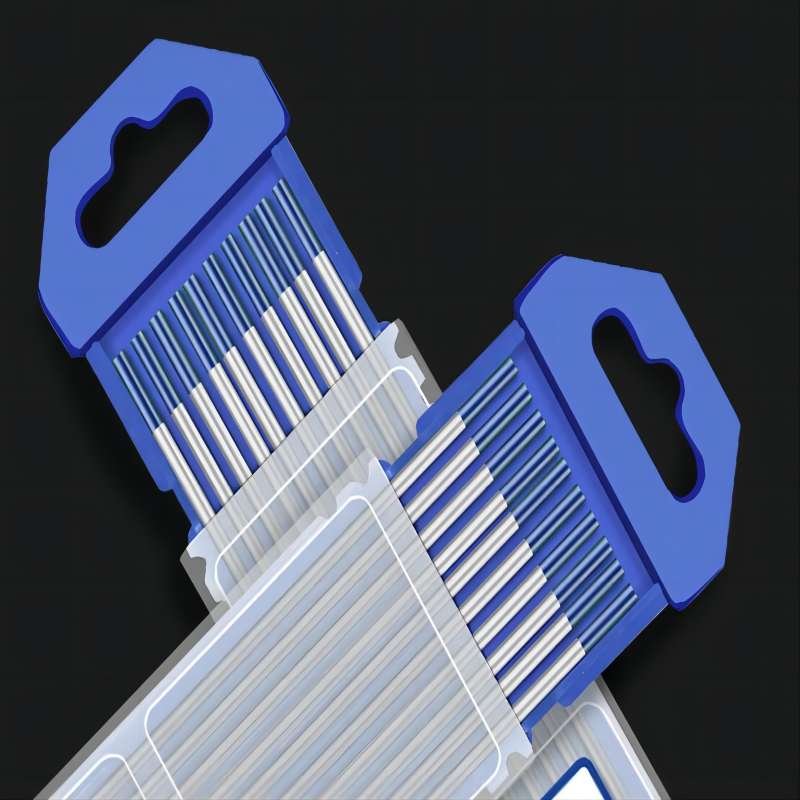
The WL20 lanthanum tungsten electrode is a type of tungsten electrode containing 2% lanthanum oxide (La2O3). Lanthanum oxide, as a rare earth additive, significantly improves the welding performance of the electrode. WL20 electrodes are typically identified by their blue-colored tip, which is the international color code used to distinguish different types of tungsten electrodes. The WL20 electrode is designed to offer a solution that is suitable for both alternating current (AC) and direct current (DC) welding applications, especially in situations requiring higher currents.
Chemical Composition
| Name | Grade | Dopant | Doping Amount | Tungsten Content % | Color Code |
| Lanthanated Tungsten Electrodes | WL20 | LaO2 | 1.80~2.20% | >96.5 | Blue |
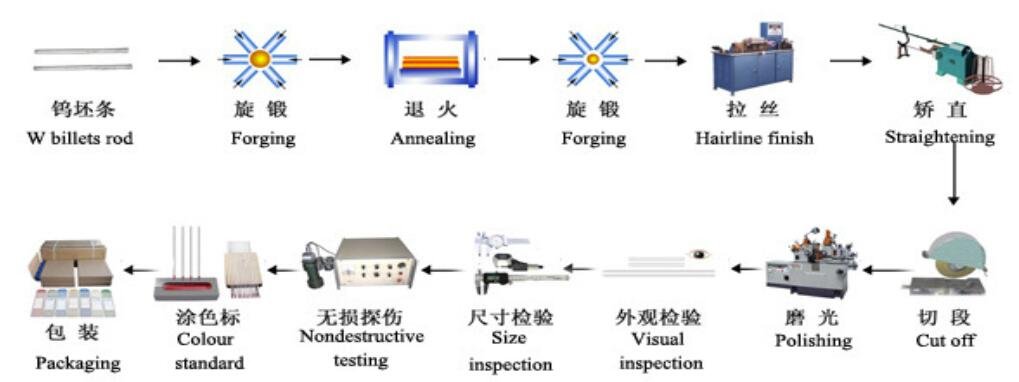
Manufacturing Process
Dimensions
| Grade | Diameter | Length |
| WL20 | 1.0mm | 150mm or 175mm or Customized |
| WL20 | 1.6mm | 150mm or 175mm or Customized |
| WL20 | 2.0mm | 150mm or 175mm or Customized |
| WL20 | 2.4mm | 150mm or 175mm or Customized |
| WL20 | 3.0mm | 150mm or 175mm or Customized |
| WL20 | 3.2mm | 150mm or 175mm or Customized |
| WL20 | 4.0mm | 150mm or 175mm or Customized |
| WL20 | 5.0mm | 150mm or 175mm or Customized |
| WL20 | 6.0mm | 150mm or 175mm or Customized |
| WL20 | 8.0mm | 150mm or 175mm or Customized |
| WL20 | 10.0mm | 150mm or 175mm or Customized |
| WL20 | 12.0mm | 150mm or 175mm or Customized |
Surface
All thoriated tungsten electrodes come with a default polished surface finish; we also offer tungsten electrodes with a black surface treatment.

(Polished)

(Black)
Advantage
(1)Superior Arc Starting: Lanthanum-containing tungsten electrodes have easy arc starting and good re-ignition properties, suitable for various welding needs.
(2)Stable Arc: In both AC and DC welding, WL20 electrodes provide a stable arc, contributing to improved welding quality.
(3)Low Burn-off Rate: Compared to traditional thorium tungsten electrodes, WL20 electrodes have a lower burn-off rate at high temperatures, thus extending the electrode's life.
(4)Non-radioactive: Being thorium-free, WL20 electrodes are a safer choice, eliminating concerns about radioactivity associated with thorium tungsten electrodes.
Disadvantages
Lanthanum tungsten electrodes are relatively expensive and not very economical; they require special equipment and processes due to the difficulty in processing; the grains tend to grow large, and the migration rate can decrease, affecting performance.
What Is Thoriated Tungsten Used For?
Lanthanum tungsten electrodes are suitable for both DC and AC welding applications, as well as for microbeam plasma welding.
Main application areas include:
.Aluminum and aluminum alloys
.Carbon Steel
.Stainless Steel
.Silicon copper
.Copper
.Titanium
Tungsten Electrode Diameter and Corresponding Amperage Table
| Dia. | DC(A) | AC(A) | |||
| in | mm | Cathode contacted(-) | Anode contacted(+) | Asymmetric waveform | Symmetric waveform |
| 0.04" | 1 | 15-80 | 10-80 | 20-60 | |
| 1/16" | 1.6 | 60-150 | 10-18 | 50-120 | 40-100 |
| 0.079" | 2 | 100-200 | 12-20 | 70-160 | 60-130 |
| 3/32" | 2.4 | 150-250 | 15-25 | 80-200 | 80-150 |
| 1/8" | 3.2 | 220-350 | 20-35 | 150-270 | 120-200 |
| 5/32" | 4 | 350-500 | 35-50 | 220-350 | 170-260 |
| 3/16" | 4.8 | 420-650 | 45-65 | 240-420 | 220-340 |
| 1/4" | 6.4 | 600-900 | 65-100 | 360-560 | 250-450 |
Package
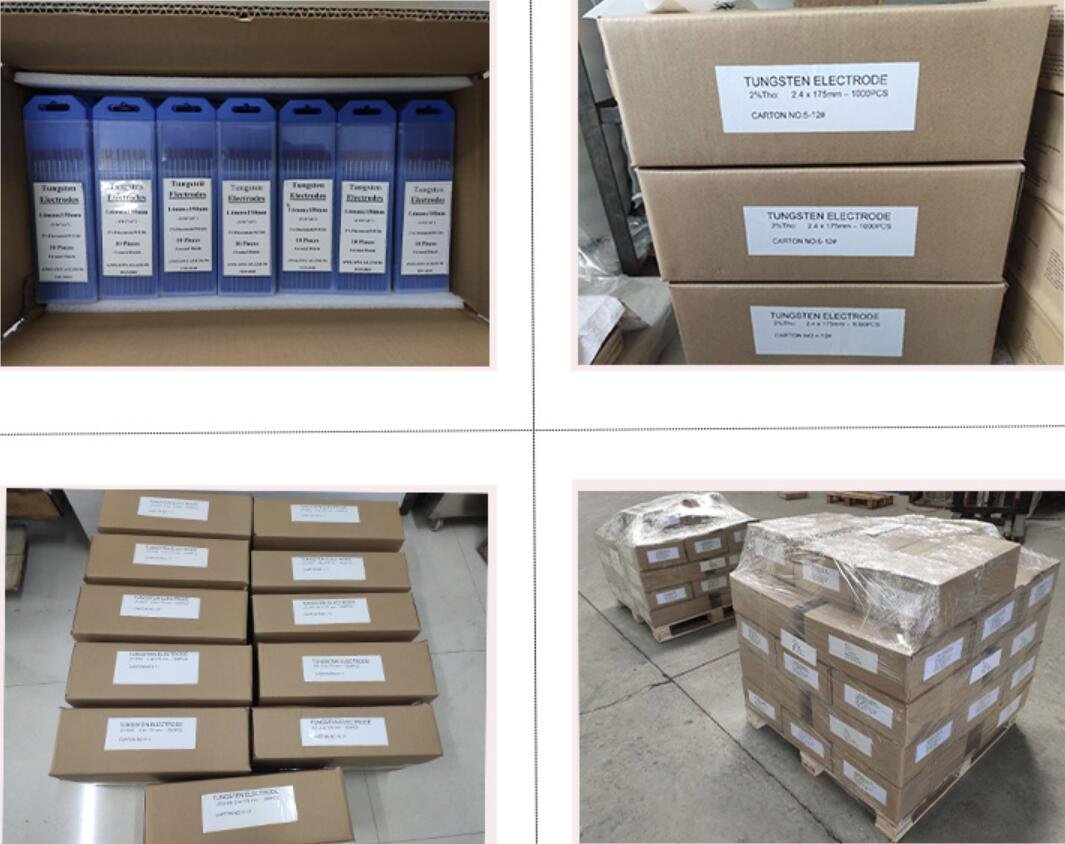
Retail Packaging: 10 pieces/plastic box

Wholesale Packaging:
.10 pieces/plastic box, 10 plastic boxes/carton, 10 cartons/case (Total: 1000 pieces/case)
.10 pieces/plastic box, 20 plastic boxes/carton, 6 cartons/case (Total: 1200 pieces/case)
Electrode Types
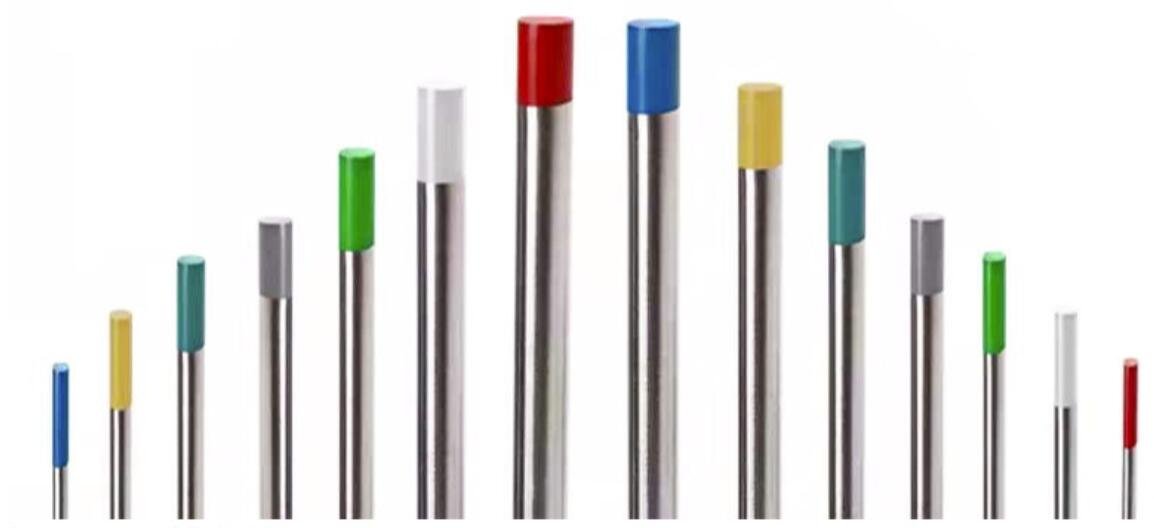
| Type of electrode | Grade | Dioxide | Dioxide in % | Impurities% | Colour Code |
| Thorium Tungsten Electrode | WT10 | ThO2 | 0.9-1.2 | <0.20 | Yellow |
| WT20 | ThO2 | 1.7-2.2 | <0.20 | Red | |
| WT30 | ThO2 | 2.8-3.2 | <0.20 | Purple | |
| WT40 | ThO2 | 3.8-4.2 | <0.20 | Orange | |
| Cerium Tungsten Electrode | WC20 | CeO2 | 1.8-2.2 | <0.20 | Grey |
| Lanthanum Tungsten Electrode | WL10 | La2O3 | 0.8-1.2 | <0.20. | Black |
| WL15 | La2O3 | 1.3-1.7 | <0.20 | Golden | |
| WL20 | LazO3 | 1.8-2.2 | <0.20 | Blue | |
| Pure Tungsten Electrode | WP | -- | -- | <0.10 | Green |
Common Issues and Precautions
1,When used after sharpening, the tip of the tungsten electrode easily breaks off cleanly.
Cause:
The use of excessive current. When tungsten electrodes are used for a long time under high current, the temperature reaches the recrystallization temperature of tungsten grains (1600°C), causing the grains to become round, coarse, and the electrode to become brittle.
Solution:
For prolonged use, the current should be close to the allowed current for the tungsten needle.
2,Arc Scattering
Cause:
A.Sharpened laterally, with grinding marks perpendicular to the electrode axis;
B. Rough grinding marks, leading to dispersed discharge points;
C. The tip does not meet requirements.
Solution:
A,Use longitudinal sharpening;
B. Use a grinding wheel with finer grains;
C. Determine the size of the sharpened tip according to the required arc concentration.
3,Arc Deviation
Cause:
A.Tungsten electrode has porosity;
B. Tungsten electrode splits;
C. Arc starting current set too high.
Solution:
A.Cut off the tip and re-sharpen;
B. Cut off the split part and re-sharpen or replace with a new tungsten electrode;
C. Set the arc starting current to about half of the upper limit of the working current.
4,Tungsten electrode forming a mushroom head?
Cause:
A.Tungsten electrode has porosity;
B. Sharpening is not concentric;
C. There's an issue with the welding torch angle.
Solution:
A.If the tungsten electrode is not straight, manually straighten it, if not possible, then replace it with the manufacturer;
B. Use a tungsten electrode with high concentricity for sharpening, and re-sharpen promptly after a mushroom head forms during the welding process;
C. Check and adjust the welding torch angle timely.
5,Tungsten electrode burns off quickly?
Cause:
A.Excessive current;
B. Inexperienced operation, tungsten electrode contacting the base material;
C. Incorrect selection of tungsten electrode, including diameter and type;
D. Tungsten electrode protruding too long;
E. Tungsten electrode sharpened too long;
F. Impure argon, leading to oxidation of the tungsten needle;
G. Argon flow too high or too low, causing the tungsten needle to contact air and oxidize at the tip.
Solution:
A.Adjust the current according to the allowed current value;
B. Become proficient in contact arc starting or use high-frequency, pulse arc starting, avoid tungsten electrode contacting the base material during welding;
C. Choose a tungsten needle with a slightly larger diameter, in AC welding, select pure tungsten electrode (green tip) or zirconium tungsten electrode (white tip);
D. Adjust the protruding length of the tungsten electrode according to argon flow and nozzle size; 5. Increase the sharpening angle appropriately. See "Guide to Tungsten Electrode Sharpening Shape and Angle";
E. Ensure argon is dry without moisture, purity above 99.9%;
F. Adjust the argon flow to a moderate level.
6,Tungsten electrode cracks, hollow core, or longitudinal splits during sharpening?
Cause:
Tungsten electrode forks or splits.
Solution:
A.Cut off the cracked part;
B. Replace with the manufacturer;
C. Perform 100% flaw detection.
7,Tungsten electrode bursting?
Cause:
A.Tungsten electrode has porosity;
B. Tungsten electrode splits;
C. Arc starting current set too high.
Solution:
A.Cut off the tip and re-sharpen;
2. Cut off the split part and re-sharpen or replace with a new tungsten electrode;
3. Set the arc starting current to about half of the working current upper limit.