
What Is Thoriated Tungsten?
Thoriated tungsten electrodes, containing thorium oxide (ThO2 or thorium dioxide), are the most commonly used electrodes for TIG welding and are widely applied in the field of DC welding. 2% thoriated tungsten electrode is a user-friendly option that performs exceptionally well even under heavy current loads. It has the lowest work function, showing excellent performance even under overloaded voltage conditions. The capabilities of thoriated tungsten electrodes surpass those of pure tungsten electrodes in many aspects. Thorium oxide provides approximately 20% higher current carrying capacity than pure tungsten, offers an extended lifespan, and aids in minimizing contamination during welding. Using thoriated tungsten electrodes facilitates easier arc initiation and yields a more stable arc compared to pure tungsten or zirconiated tungsten electrodes.
Chemical Composition
| Name | Dopant | Doping Amount | Tungsten Content % | Color Code |
| Thoriated Tungsten Electrodes | ThO2 | 1.80~2.20% | >97.5 | Red |
Dimensions
| Grade | Diameter | Length |
| WT20 | 1.0mm | 150mm or 175mm or Customized |
| WT20 | 1.6mm | 150mm or 175mm or Customized |
| WT20 | 2.0mm | 150mm or 175mm or Customized |
| WT20 | 2.4mm | 150mm or 175mm or Customized |
| WT20 | 3.0mm | 150mm or 175mm or Customized |
| WT20 | 3.2mm | 150mm or 175mm or Customized |
| WT20 | 4.0mm | 150mm or 175mm or Customized |
| WT20 | 5.0mm | 150mm or 175mm or Customized |
| WT20 | 6.0mm | 150mm or 175mm or Customized |
| WT20 | 8.0mm | 150mm or 175mm or Customized |
| WT20 | 10.0mm | 150mm or 175mm or Customized |
| WT20 | 12.0mm | 150mm or 175mm or Customized |
Surface
All thoriated tungsten electrodes come with a default polished surface finish; we also offer tungsten electrodes with a black surface treatment.
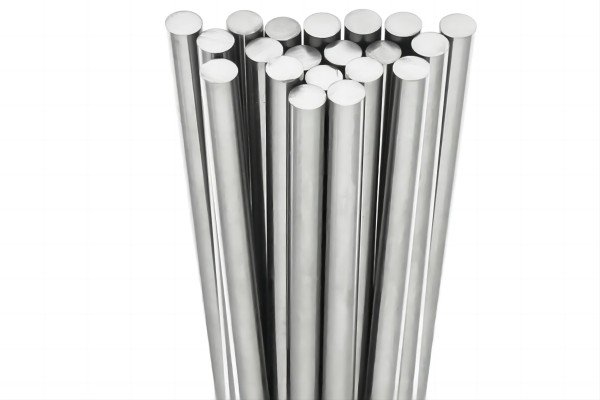
(Polished)
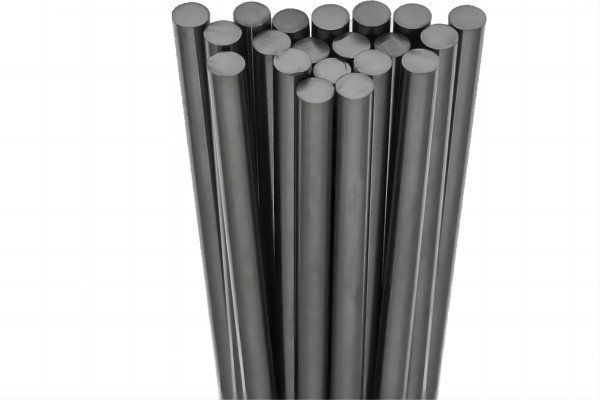
(Black)
Advantage
.High surface glossiness, free of burrs
.Good electrical conductivity, easy arc initiation, and stable arc
.Long welding life and high wear resistance
.Low melting rate, time-saving and efficient
Disadvantages
Due to the presence of thorium, there is slight radioactive contamination. It is essential to maintain good ventilation when welding with thoriated tungsten electrodes, and the disposal of used welding tips must be handled properly.
What Is Thoriated Tungsten Used For?
For DC welding of base materials such as:
.Carbon steel
.Stainless steel
.Nickel alloys
.Titanium alloys
.Iron
Tungsten Electrode Diameter and Corresponding Amperage Table
| Dia. | DC(A) | AC(A) | |||
| in | mm | Cathode contacted(-) | Anode contacted(+) | Asymmetric waveform | Symmetric waveform |
| 0.04" | 1 | 15-80 | 10-80 | 20-60 | |
| 1/16" | 1.6 | 60-150 | 10-18 | 50-120 | 40-100 |
| 0.079" | 2 | 100-200 | 12-20 | 70-160 | 60-130 |
| 3/32" | 2.4 | 150-250 | 15-25 | 80-200 | 80-150 |
| 1/8" | 3.2 | 220-350 | 20-35 | 150-270 | 120-200 |
| 5/32" | 4 | 350-500 | 35-50 | 220-350 | 170-260 |
| 3/16" | 4.8 | 420-650 | 45-65 | 240-420 | 220-340 |
| 1/4" | 6.4 | 600-900 | 65-100 | 360-560 | 250-450 |
Package
Retail Packaging: 10 pieces/plastic box
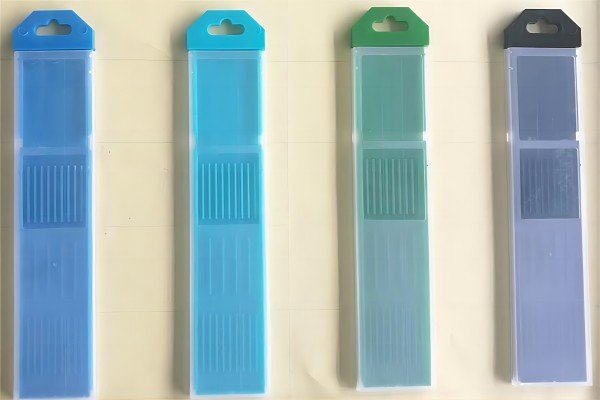
Wholesale Packaging:
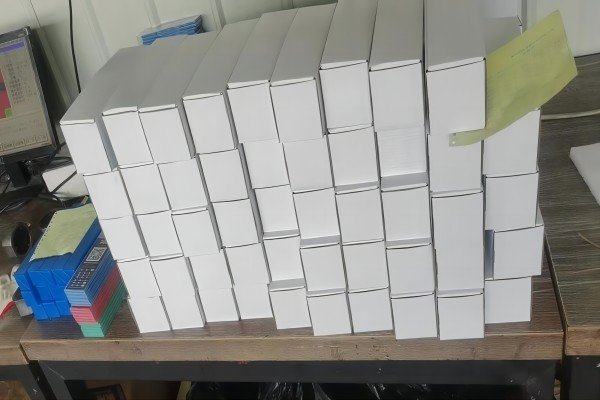
1000 pieces per case
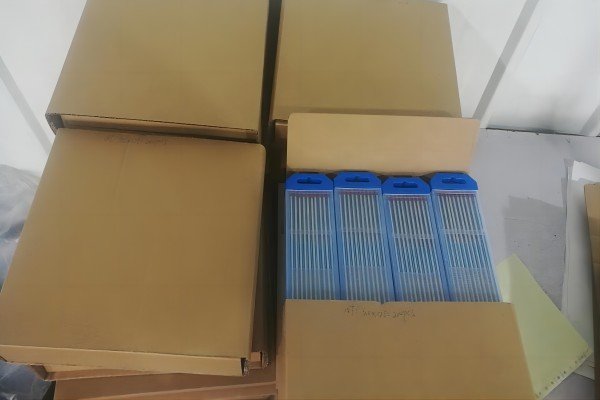
1200 pieces per case
Common Issues and Precautions
| 1,Tungsten Inclusion in TIG Welding | |
| Cause | Prevention Measures |
| Initiating arc by contacting the workpiece leading to tungsten electrode melting | Use a high-frequency oscillator and high-voltage pulse generator for arc initiation |
| Reduce current or increase tungsten electrode diameter to decrease electrode protrusion length | |
| Replace any tungsten electrode with cracks | |
| 2,Poor Gas Shielding | |
| Cause | Prevention Measures |
| Workpieces and filler wire contaminated by oxygen/nitrogen/air/moisture | Use argon gas with a purity of 99.99% |
| Ensure adequate pre-flow and post-flow time | |
| Perform thorough cleaning before welding | |
| Choose the correct gas flow rate/nozzle size/electrode protrusion length | |
| 3,Unstable Arc | |
| Cause | Prevention Measures |
| Oil contamination on the workpiece | Perform thorough cleaning before welding |
| Joint bevel too narrow | Widen the bevel and shorten the arc length |
| Tungsten electrode contamination | Remove contaminated parts |
| Tungsten electrode diameter too large | Choose the correct tungsten electrode |
| Arc length too long | Reduce nozzle distance |
| 4,Excessive Tungsten Electrode Wear | |
| Cause | Prevention Measures |
| Poor gas shielding leading to tungsten electrode oxidation | Clean the nozzle and slightly increase gas flow |
| Tungsten electrode diameter too small | Increase tungsten electrode diameter |
| Tungsten electrode oxidized when stopping welding | Increase post-flow time |
Related Articles